 REPRESENTATIVE CONCEPT
Under Development
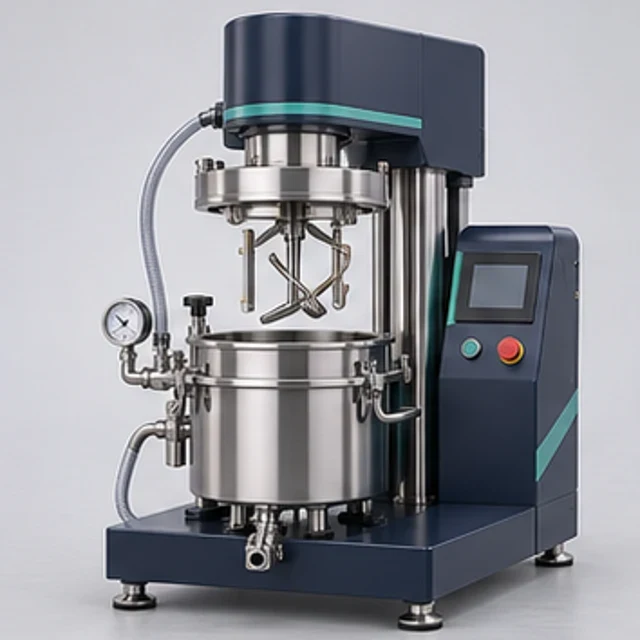
Laboratory Vacuum Planetary Mixer
Li-ion Laboratory EquipmentLaboratory slurry mixing under controlled pressure.
AMB-LPM-05Explore equipment ↗
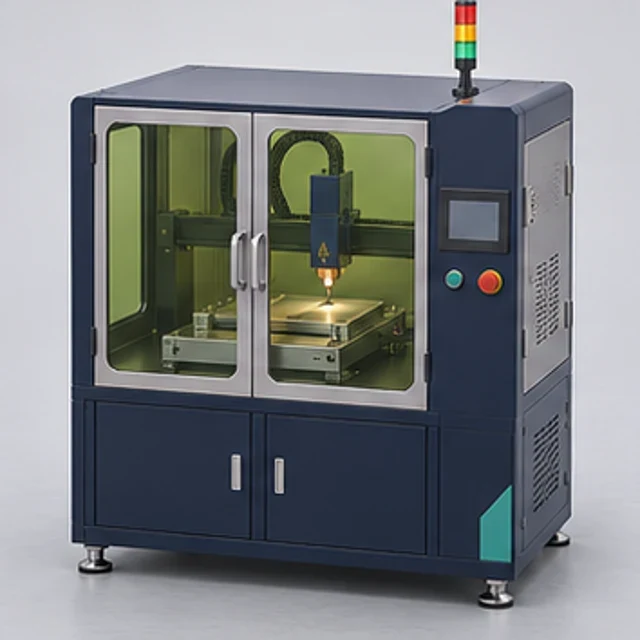
Intended for trials joining compatible tab and current-collector materials, where joint design, foil stack and damage limits need qualification using representative samples.
| Parameter | Indicative Configuration |
|---|---|
| Equipment type | Ultrasonic Battery Tab Welding Machine |
| Welding principle | Ultrasonic metal welding |
| Operating frequency | 20 kHz standard reference class |
| Alternative frequency | 40 kHz, suitable selected equipment |
| Ultrasonic power class | 1 / 2 / 3 kW |
| Generator | Digital ultrasonic generator |
| Frequency tracking | Automatic, selected generator |
| Amplitude adjustment | Programmable, selected system |
| Welding mode | Time / energy / optional power control |
| Welding duration | Process-dependent; subject to selected system and welding trials |
| Weld area | Application-specific horn/tooling contact; subject to process trials |
| Welding horn | Application-specific sonotrode |
| Anvil | Precision-machined / hardened tool |
| Weldable materials | Aluminium / copper / nickel combinations, subject to trials |
| Foil-stack capacity | Based on foil thickness, material and welding trials |
| Tab geometry | Customer-specific |
| Clamping mechanism | Pneumatic |
| Pneumatic supply | 0.5–0.8 MPa reference class |
| Welding force | Controlled, application-dependent |
| Fixture arrangement | Manual loading / sliding fixture |
| Station arrangement | Single or dual station |
| Positioning | Adjustable mechanical fixture |
| Controller | Digital HMI / supplier controller |
| Recipe storage | Selected system capability |
| Weld monitoring | Energy / time / displacement, where supported |
| Data logging | Optional |
| Electrical supply | 220–240 V AC single-phase or supplier-approved configuration |
| Safety | Guarding, interlocks, controlled actuation and emergency stop |
| Fume/debris control | Suitable extraction provision |
| Applications | Li-ion pouch/cylindrical-cell tab and foil-stack joining |
Technical configurations are indicative and subject to application requirements. Final equipment selection, specifications, performance and supply arrangements will be confirmed during technical evaluation and quotation.
Model labels and power/frequency classes are proposed sourcing options, subject to supplier availability and process trials. They do not establish validated welding output or a universal foil-stack capacity. Frequency, generator, horn, anvil, power and clamping must be matched to the actual tab material, geometry and stack. Weld strength, electrical resistance and appearance require process validation.
AMPLEMECH offers configurable ultrasonic tab welding solutions for battery laboratory and pilot applications, combining application-specific fixtures, automation integration and specialised ultrasonic welding technology selected according to customer requirements. Mechanical vibration under controlled clamping joins selected metal interfaces. The ultrasonic generator, transducer, booster, horn and qualified tooling require a compatible selected system; this listing does not establish in-house manufacture of ultrasonic electronics.
Tab-to-foil joining studies, research-cell preparation and pilot joint-process development. Confirm the intended process, materials and acceptance method during application review.
Mechanical interfaces, operating mode and control requirements are defined during engineering review. Available configuration choices depend on the agreed equipment scope.
A selected supplier controller or digital HMI supports the agreed weld modes and recipes. Power control, displacement monitoring, data logging and automation integration are optional and require selected-system support.
Equipment configuration and specialised subsystems are selected according to application requirements, with engineering integration and supply feasibility confirmed during technical evaluation. Utilities and facility interfaces depend on the selected equipment. This enquiry-led listing does not establish stock, immediate dispatch, completed installations, in-house manufacture of specialist instruments or a confirmed supplier relationship.
Weld strength, electrical resistance, foil-stack capacity and visual acceptance require actual material/thickness trials. Horn and anvil geometry, frequency, power, clamping and process settings require matching and validation. Guarding, interlocks, emergency isolation, pneumatic safety, noise and fume/debris extraction require assessment. Proprietary competitor mechanisms or tooling must not be reproduced. Supplier certification does not automatically certify an integrated machine; no assembled-system approval is established.
A documented risk assessment, guarding review, material compatibility check and application-specific operating procedure are required before use. No CE, UL, IEC, hazardous-area approval or other certification is established by this listing. Conformity documentation depends on the agreed scope and destination requirements.
Read the Product Information Disclaimer
Request technical documentation and an application-specific configuration with your enquiry.
This listing represents an intended equipment or engineering offering. Feasibility, configuration and availability require confirmation. Please request the current engineering and supply status.
Share your materials, required capacity, process constraints and acceptance criteria. The team will review feasibility before confirming any custom scope.
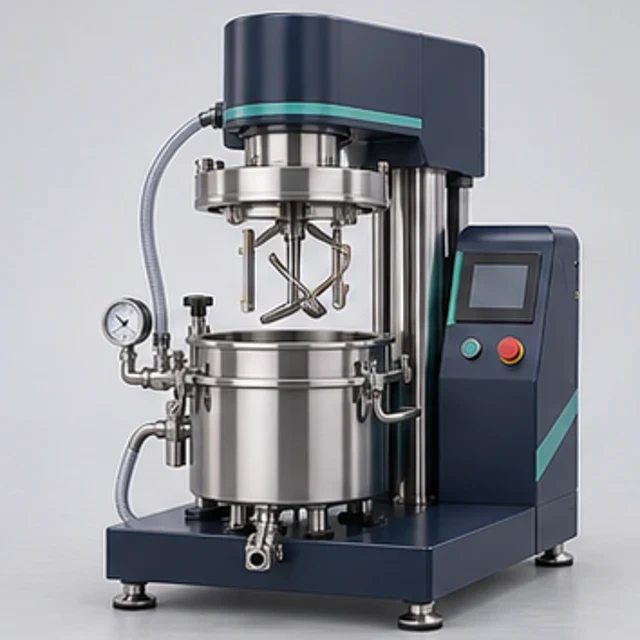
REPRESENTATIVE CONCEPTLaboratory slurry mixing under controlled pressure.
 REPRESENTATIVE CONCEPT
Laboratory rotor-stator dispersion.
 REPRESENTATIVE CONCEPT
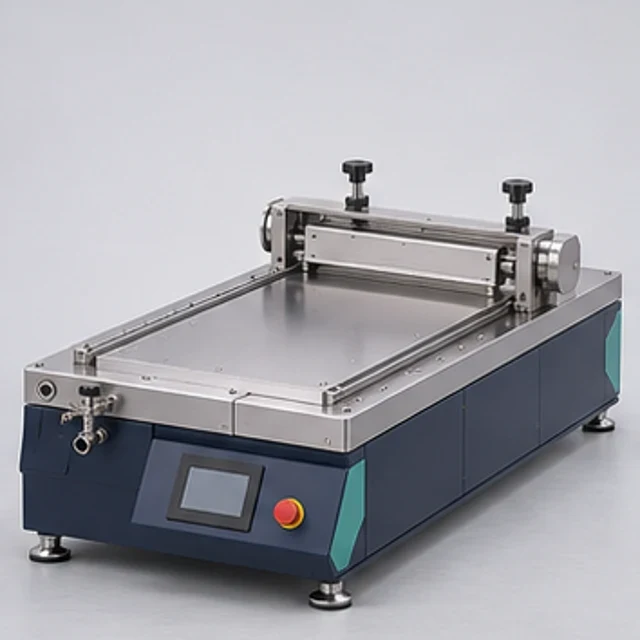
Laboratory blade coating of electrode coupons.