 REPRESENTATIVE CONCEPT
Planned
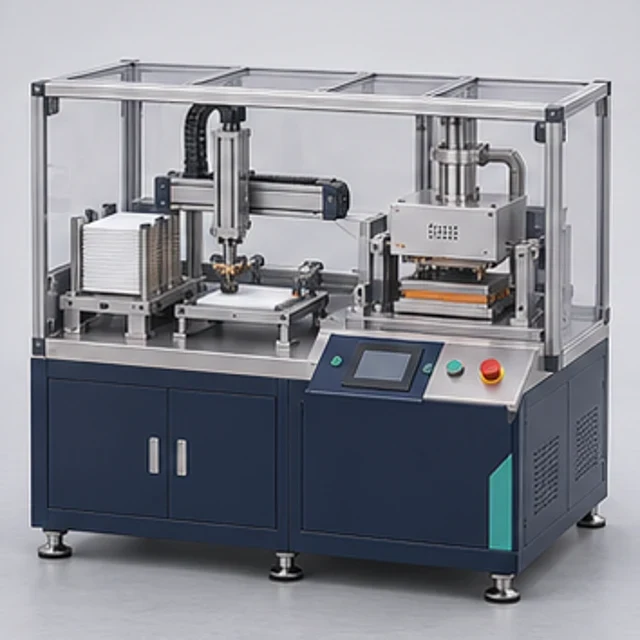
Prismatic Cell Stacking or Flat-Winding Machine
Li-ion Prismatic Cell EquipmentPrismatic electrode assembly route review.
AMB-PRS-100Explore equipment ↗
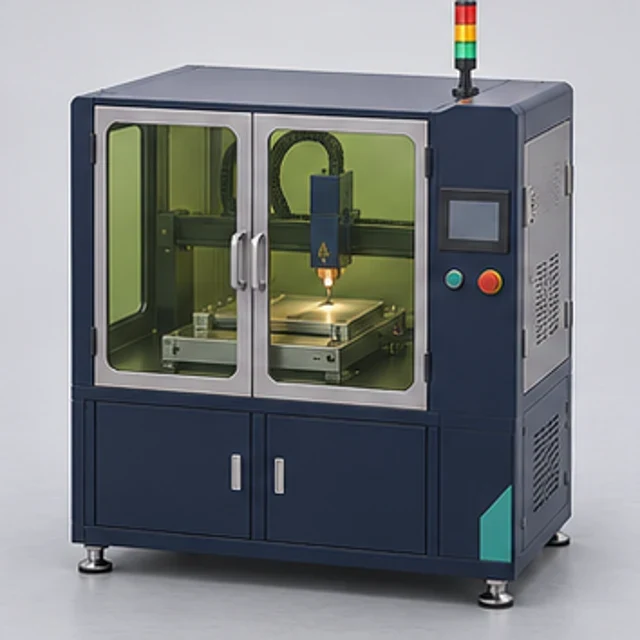
Intended for supplier and engineering review of laser welding at specified prismatic-cell joints, with enclosure alloys, fit-up and sensitive internal components defined before trials.
| Technical Parameter | Indicative Configuration |
|---|---|
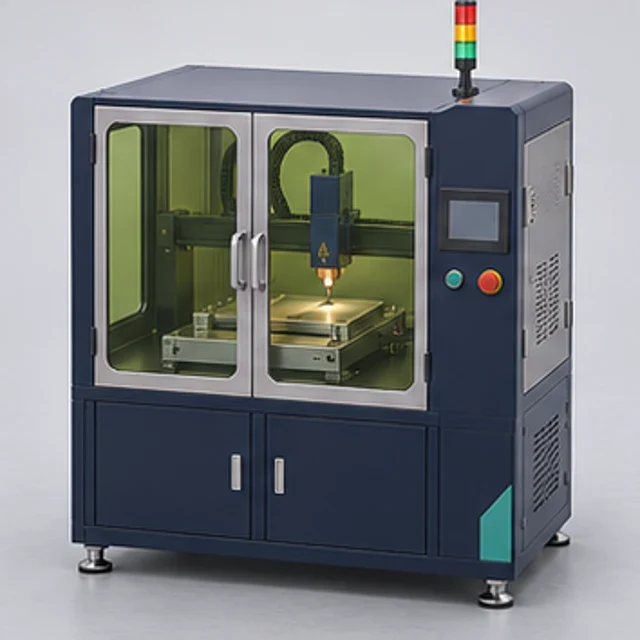
| Equipment type | Prismatic Cell Laser Welding & Sealing System |
| Intended application | Prismatic-cell laser closure/joining review |
| Process principle | A focused laser beam heats the defined joint to create a weld according to a qualified path. Absorption, joint gap, shielding and heat flow influence seam quality; a laser system does not automatically establish a leak-tight or certified cell. |
| Proposed configurations | Lid seam / Tab connection / Enclosed custom station |
| Joint | Actual material pair, coatings, thickness and joint design |
| Technology | Selected specialist laser joining system |
| Source | Selected laser source and compatible optics; no in-house source claim |
| Tool/optics | Joint-specific beam delivery, focus and fixture access |
| Access | Custom fixture and tool/beam clearance |
| Clamping | Joint-specific controlled force/restraint |
| Heat/energy | Selected source and qualified process programme |
| Monitoring | Optional selected weld signals/inspection |
| Protection | Process-specific enclosure, guarding and extraction |
| Joint acceptance | Actual sample strength, resistance and damage checks |
| Sizing and capacity basis | Application-specific; finalised after technical review. Relevant units: mm; W source-specific; mm/s; µΩ or leak rate by method. No rating is inferred from the machine ID. |
| Control architecture | Selected process/instrument controls; integration PLC/HMI only where justified by the agreed scope. |
| Utilities and installation | Power, air/hydraulics, thermal services and exhaust only as applicable to the selected scope; site requirements confirmed in the technical offer. |
| Service and configuration changes | Accessible service interfaces and controlled tooling/recipe changes for the agreed process; cleaning/contamination requirements application-specific. |
| Safety and process limits | Laser radiation, spatter, vapours and supplier certification not automatically system conformity. Safeguards and required conformity route need competent application-specific assessment. |
| Acceptance basis | Agreed drawings/material samples and measurable process acceptance for joint/material; laser source; seam; heat limit; monitoring; leak acceptance. Actual trials and selected-component evidence required before a performance commitment. |
Technical specifications are indicative and configurable. Final equipment parameters, performance, compatibility and supply arrangements will be confirmed following application review and detailed engineering.
Configurations are alternatives or separately selected options, not universal inclusions. Final scope depends on the actual process, materials and selected components; no capacity, precision, yield, delivery or certification is established by this listing.
Equipment configurations and specialised technologies selected according to project requirements, with supply feasibility confirmed during technical evaluation. A focused laser beam heats the defined joint to create a weld according to a qualified path. Absorption, joint gap, shielding and heat flow influence seam quality; a laser system does not automatically establish a leak-tight or certified cell. The exact selected configuration and supply feasibility are established after enquiry qualification; this is not an assertion of completed manufacture or available stock.
Prismatic cap/seam development and trials of specified metal connections in a controlled assembly process. Confirm the intended process, materials and acceptance method during application review.
Mechanical interfaces, operating mode and control requirements are defined during engineering review. Available configuration choices depend on the agreed equipment scope.
Standard and optional operations are separated in the technical offer. Specialist technology, instrumentation and safety functions require selected-equipment evidence and appropriate integration validation.
Installation scope and facility responsibilities are agreed for the actual process. No unselected utility plant, environmental-control system, process recipe or complete turnkey facility is automatically included.
Laser radiation, spatter, vapours and supplier certification not automatically system conformity. Configurations are alternatives or separately selected options, not universal inclusions. Final scope depends on the actual process, materials and selected components; no capacity, precision, yield, delivery or certification is established by this listing. No verified performance, supplier appointment or certification is established by this catalogue entry.
A documented risk assessment, guarding review, material compatibility check and application-specific operating procedure are required before use. No CE, UL, IEC, hazardous-area approval or other certification is established by this listing. Conformity documentation depends on the agreed scope and destination requirements.
Read the Product Information Disclaimer
Request technical documentation and an application-specific configuration with your enquiry.
Intended partner-supply route only. No named partner appointment, authorisation, available machine, scope or delivery is confirmed by this listing. Please request the current engineering and supply status.
Share your materials, required capacity, process constraints and acceptance criteria. The team will review feasibility before confirming any custom scope.
REPRESENTATIVE CONCEPTPrismatic electrode assembly route review.
 REPRESENTATIVE CONCEPT
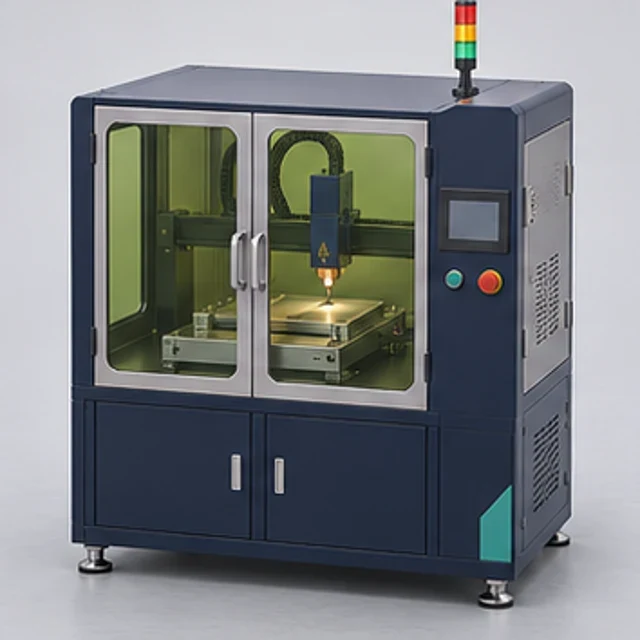
Laboratory ultrasonic joining of cell tabs.
 REPRESENTATIVE CONCEPT
Spot or projection joining for cylindrical cells.