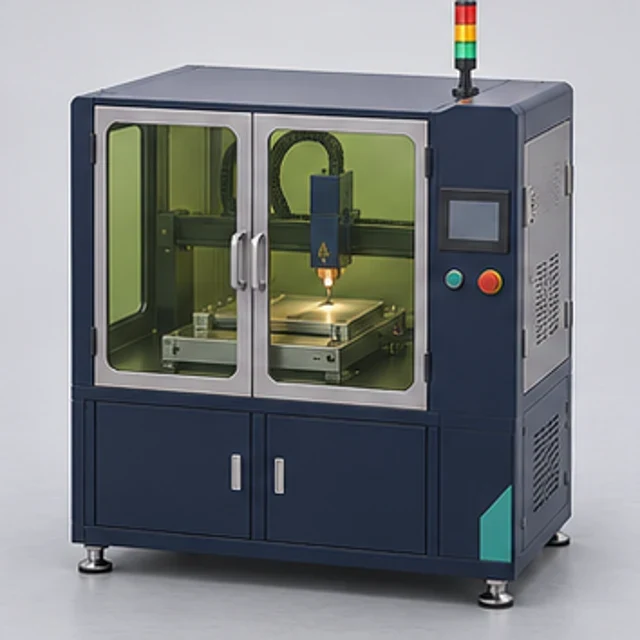
 REPRESENTATIVE CONCEPT
Planned
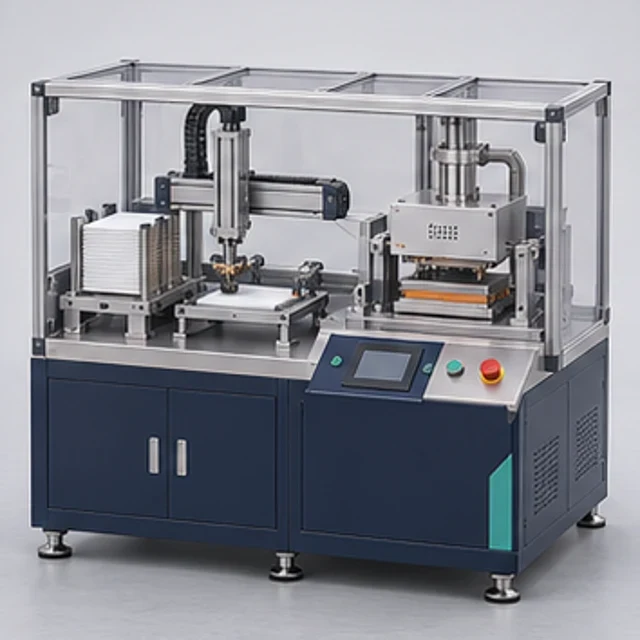
Inter-Cell Welding / Partition Welding Machine
Lead-Acid Battery AssemblyLead-acid inter-cell joining.
AMB-ICW-01Explore equipment ↗
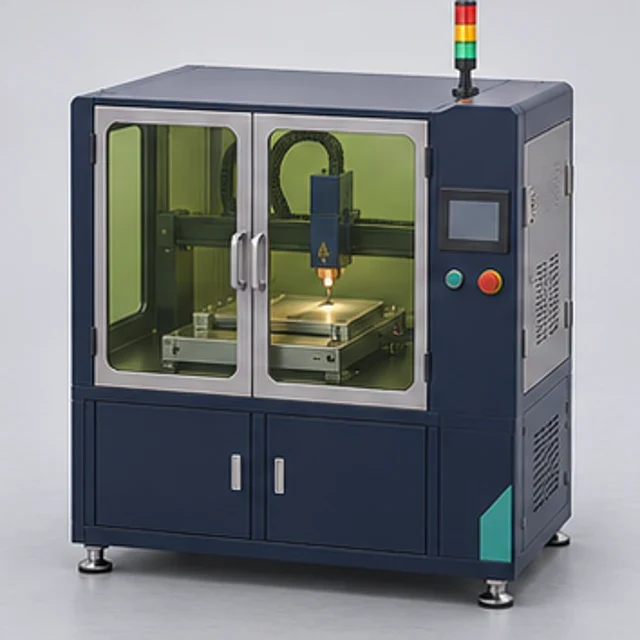
Intended for qualification of the specified lead-acid terminal/post connection, with the joining route selected from the material and enclosure design.
| Technical Parameter | Indicative Configuration |
|---|---|
| Equipment type | Terminal / Post Welding Machine |
| Intended application | Lead-acid terminal and post joining |
| Process principle | A controlled joining process creates a conductive connection while tooling supports the terminal and adjacent seal. Heat/current distribution and lead-alloy condition affect joint strength and leakage risk. |
| Proposed configurations | Selected resistance route / Custom thermal joint / Tooling option |
| Joint | Customer connector/post/lug and case geometry |
| Alloys | Declared lead/connector composition and surface condition |
| Process | Selected qualified joining route, not universal material capability |
| Positioning | Custom support and locating fixtures |
| Actuation | Controlled clamping and protected approach |
| Energy/heat | Selected source and joint-specific programme |
| Insulation | Protection of case partitions, seals and nearby components |
| Fume control | Local capture and lead-residue containment interface |
| Monitoring | Optional selected current/force/process records |
| Acceptance | Agreed electrical resistance and mechanical joint tests |
| Sizing and capacity basis | Application-specific; finalised after technical review. Relevant units: mm; A/J process-specific; N; µΩ; s. No rating is inferred from the machine ID. |
| Control architecture | Selected process/instrument controls; integration PLC/HMI only where justified by the agreed scope. |
| Utilities and installation | Power, air/hydraulics, thermal services and exhaust only as applicable to the selected scope; site requirements confirmed in the technical offer. |
| Service and configuration changes | Accessible service interfaces and controlled tooling/recipe changes for the agreed process; cleaning/contamination requirements application-specific. |
| Safety and process limits | Lead fumes, shorts, seal damage and no universal post-weld capability. Safeguards and required conformity route need competent application-specific assessment. |
| Acceptance basis | Agreed drawings/material samples and measurable process acceptance for post/terminal alloys; joint geometry; heat/current; force; resistance; integrity. Actual trials and selected-component evidence required before a performance commitment. |
Technical specifications are indicative and configurable. Final equipment parameters, performance, compatibility and supply arrangements will be confirmed following application review and detailed engineering.
Configurations are alternatives or separately selected options, not universal inclusions. Final scope depends on the actual process, materials and selected components; no capacity, precision, yield, delivery or certification is established by this listing.
Application-specific machinery combining mechanical engineering, automation integration and selected specialist subsystems. A controlled joining process creates a conductive connection while tooling supports the terminal and adjacent seal. Heat/current distribution and lead-alloy condition affect joint strength and leakage risk. The exact selected configuration and supply feasibility are established after enquiry qualification; this is not an assertion of completed manufacture or available stock.
Lead-acid terminal connection trials and development of a defined post-to-connector assembly process. Confirm the intended process, materials and acceptance method during application review.
Mechanical interfaces, operating mode and control requirements are defined during engineering review. Available configuration choices depend on the agreed equipment scope.
Standard and optional operations are separated in the technical offer. Specialist technology, instrumentation and safety functions require selected-equipment evidence and appropriate integration validation.
Installation scope and facility responsibilities are agreed for the actual process. No unselected utility plant, environmental-control system, process recipe or complete turnkey facility is automatically included.
Lead fumes, shorts, seal damage and no universal post-weld capability. Configurations are alternatives or separately selected options, not universal inclusions. Final scope depends on the actual process, materials and selected components; no capacity, precision, yield, delivery or certification is established by this listing. Lead-bearing material, dust, fumes, contaminated liquids and waste require competent exposure, containment and disposal assessment. No verified performance, supplier appointment or certification is established by this catalogue entry.
A documented risk assessment, guarding review, material compatibility check and application-specific operating procedure are required before use. No CE, UL, IEC, hazardous-area approval or other certification is established by this listing. Conformity documentation depends on the agreed scope and destination requirements.
Read the Product Information Disclaimer
Request technical documentation and an application-specific configuration with your enquiry.
This listing represents an intended equipment or engineering offering. Feasibility, configuration and availability require confirmation. Please request the current engineering and supply status.
Share your materials, required capacity, process constraints and acceptance criteria. The team will review feasibility before confirming any custom scope.
REPRESENTATIVE CONCEPTLead-acid inter-cell joining.
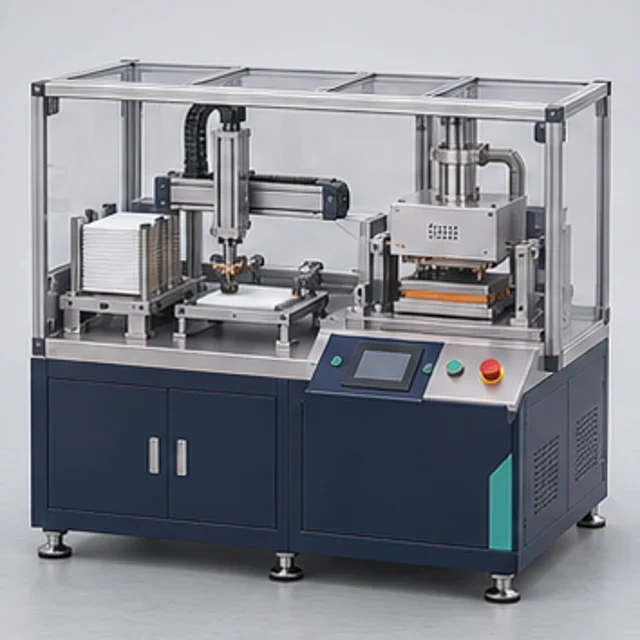 REPRESENTATIVE CONCEPT
Lead-acid plate wrapping and stack preparation.
 REPRESENTATIVE CONCEPT
Lead-acid plate enveloping and group stacking.